

Key Differences Between Hot and Cold Rolling Working Conditions
Before selecting rolling components, it is essential to understand the distinct working environments of hot rolling and cold rolling lines, as these differences determine roll material, hardness and structural requirements. Hot rolling processes high-temperature steel strips above 1000℃, exposing rolls to extreme heat, thermal shock, and heavy oxide abrasion. The core demand here is excellent thermal stability and anti-cracking performance.
In contrast, cold rolling forms steel at room temperature, requiring ultra-high surface smoothness and uniform hardness to guarantee precise strip flatness and surface quality. Cold rolling rolls bear continuous high contact pressure, making wear resistance and surface toughness the top priorities. A one-size-fits-all selection method always leads to premature failure and unstable rolling results.
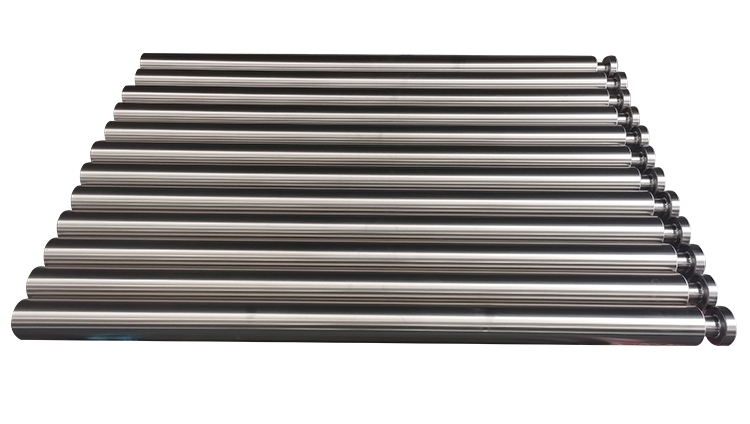
Standard Performance Parameters for Wear-Resistant Mill work roll
Professional steel mill roll selection relies on standardized industrial parameters rather than subjective experience. The following data summarizes mainstream specifications adopted by top rolling equipment manufacturers and material suppliers, covering core indicators for hot and cold rolling applications to support accurate purchasing and matching.
Performance Parameter | Hot Rolling Standard Value | Cold Rolling Standard Value | Practical Benefit |
|---|---|---|---|
Surface Hardness | HS 60–70 | HS 90–98 | Ensures anti-wear ability matching different rolling pressure levels |
Main Material Grade | Semi-steel, High Chromium Cast Iron | Cr5/ Cr6 Forged Steel, High Speed Steel | Balances thermal resistance, surface finish and impact toughness |
Effective Hardened Layer Depth | 8–12mm | 15–25mm | Supports repeated grinding and long service cycles |
Allowable Rolling Pressure | 1800–2500 MPa | 2500–3500 MPa | Avoids surface peeling and plastic deformation under heavy load |
Typical Service Life | 8000–12000 tons rolling volume | 15000–25000 tons rolling volume | Reduces replacement frequency and production interruption |

Core Selection Principles for Wear-Resistant mill work roll
1. Match Material Grade with Rolling Process
Material selection is the foundation of wear resistance. For hot rolling production lines, high chromium centrifugal cast iron and semi-steel rolls are ideal choices, featuring outstanding thermal crack resistance and oxidation resistance to cope with high-temperature rolling environments. For precision cold rolling lines, Cr5 and Cr6 forged steel rolls or high-speed steel rolls are more suitable, providing ultra-high hardness and deep hardened layers to maintain consistent strip surface quality after long-hour operation.
2. Prioritize Reasonable Hardness Matching
Many buyers mistakenly believe higher hardness always means better performance. Excessively hard rolls lack toughness and may crack under thermal shock in hot rolling scenarios. For cold rolling, insufficient hardness will quickly cause surface wear, scratches and uneven strip thickness. Adopting process-matched hardness standards ensures both wear resistance and structural stability during continuous industrial operation.
3. Verify Hardened Layer Depth and Grinding Tolerance
A qualified mill work roll must have a uniform and sufficiently thick hardened layer. Sufficient hardened depth allows multiple professional grindings after surface wear, greatly extending the overall service life. Rolls with thin or uneven hardened layers fail rapidly after repeated grinding, leading to increased long-term procurement and maintenance costs for steel mills.
4. Inspect Surface Finish and Internal Defects
Before formal installation, conduct basic quality inspection, including surface smoothness, no microscopic cracks, and uniform metallographic structure. High-quality rolls feature fine and dense internal texture, effectively resisting fatigue wear under continuous high-pressure rolling, which is critical for stabilizing finished steel product quality.
FAQs About Mill Work Roll Selection for Hot & Cold Rolling
1. What is the biggest difference between hot and cold rolling work rolls?
Hot rolling rolls focus on thermal stability and anti-cracking performance to adapt to high-temperature steel rolling and thermal shock. Cold rolling rolls prioritize ultra-high hardness, deep hardened layers and precise surface finish to meet strict flatness and smoothness requirements of finished steel strips. Their material formulas and hardness parameters are completely different and cannot be used interchangeably.
2. Which material offers the best wear resistance for cold rolling lines?
Cr5 and Cr6 forged steel materials are the most cost-effective and widely used options for standard cold rolling lines. For high-precision, high-yield production scenarios, high-speed steel rolls deliver superior wear resistance and longer service cycles, effectively reducing roll replacement frequency and improving production continuity.
3. Why do new rolls still produce steel strip surface scratches?
Surface scratches are usually caused by unqualified surface finish, uneven hardened layers, or tiny residual impurities on the roll surface. In some cases, mismatched roll hardness also leads to inconsistent friction during rolling. Professional pre-installation grinding and parameter verification can effectively solve such quality problems.
4. How to extend the service life of rolling work rolls?
First, select rolls that precisely match your rolling process parameters. Second, implement regular surface inspection and professional grinding maintenance. Finally, stabilize rolling pressure and avoid long-term overload operation. Standardized operation and maintenance can increase roll service life by 20% to 35% on average.
 Contact person:Mr.Wu
 Phone:+86 18602539156
 Email:wuqi231138@126.com
This website uses cookies to ensure you get the best experience on our website.
 Español
 Pусский
 Indonesia
 Tiếng Việt


Comment
(0)